
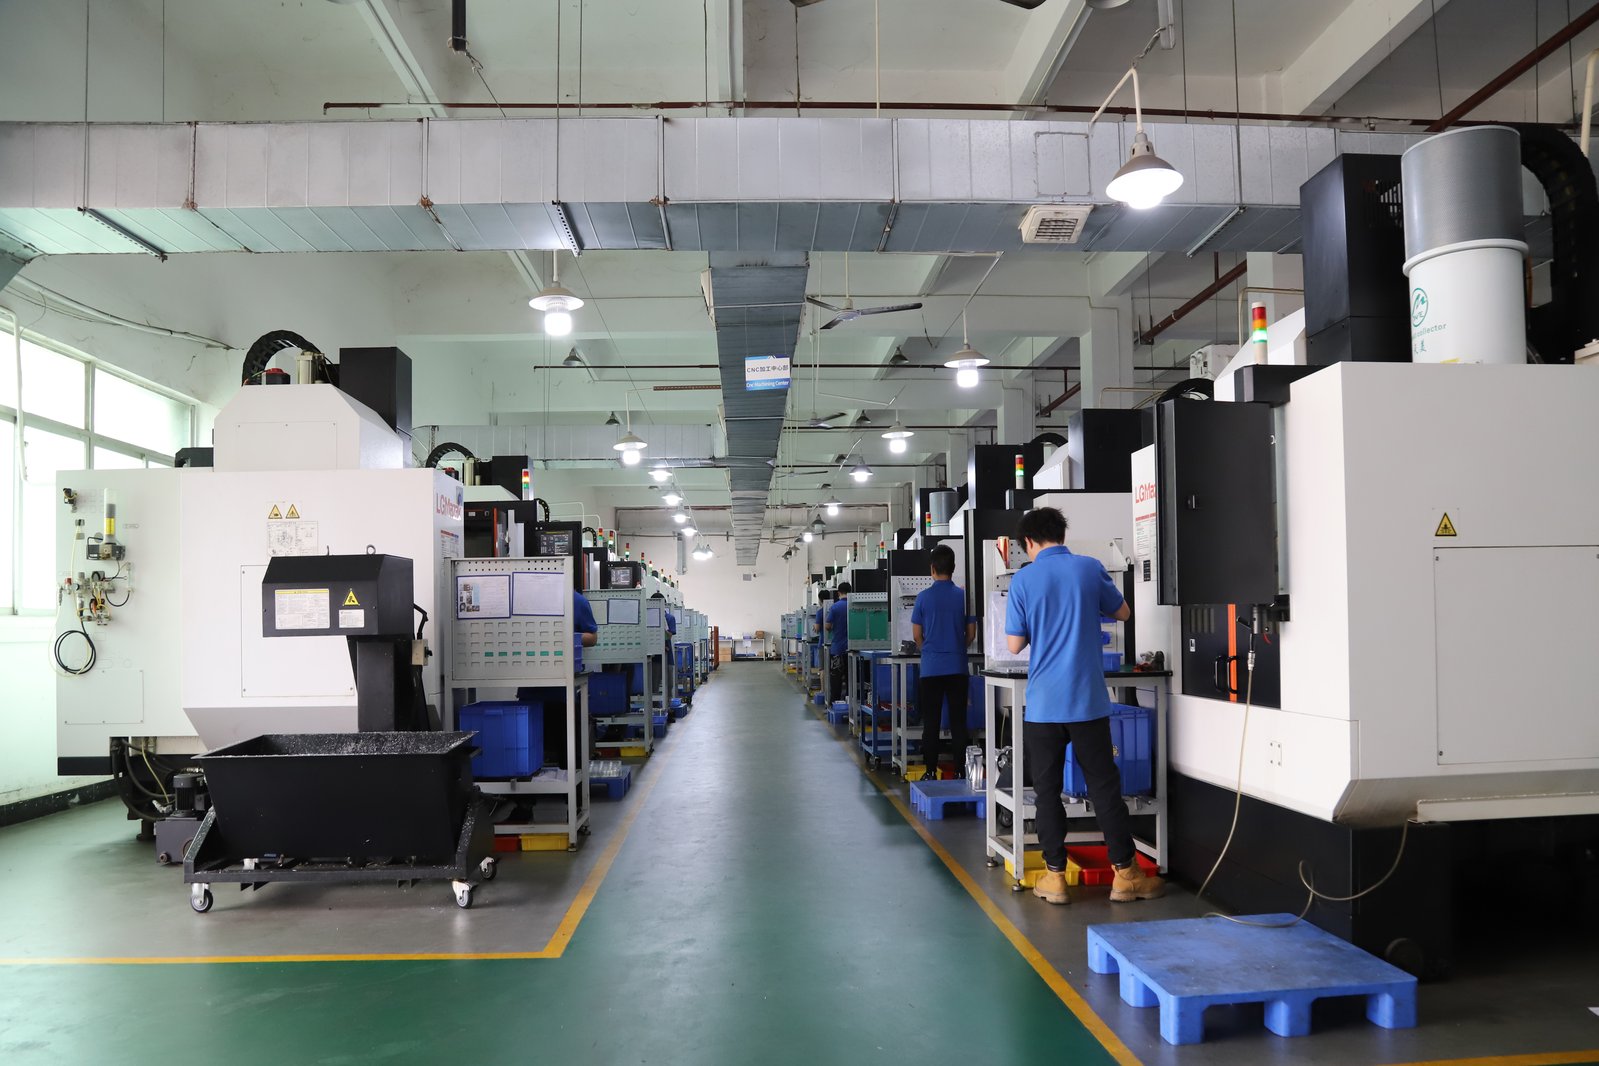
Aerospace custom components — brackets, housings, fittings, shafts, and actuator parts machined to a buyer's drawing — are not bought on geometry alone. The part is only as good as its paper trail: the material certificate tied to the heat, the first article proving every characteristic was measured, and the lot record that connects the finished component back to the metal and the machine that made it. When custom components are manufactured in China, none of that trail is harder to get, but all of it is harder to get late, which is why the buyer's job is to make documentation a deliverable of the order from the first RFQ. This article is the checklist for that trail.
What makes an aerospace component "custom" in a way that matters to a buyer?
A custom component is built to print: your drawing, your material, your quantity. In aerospace, that drawing is usually the product of a long design chain — requirements flowed down from the airframer through a tiered supply chain — and by the time it reaches a machine shop, every decision that could be made has been made. What the shop must add is execution discipline: buying the right stock, running the right process, measuring the right features, and recording everything so that the component can be traced and defended years later.
That is why the supplier relationship on aerospace custom components is a documentation relationship before it is a machining one. The components themselves are made every day in China to drawing — the machine tools are capable and the tolerances are achievable. What separates suppliers is whether the certificate arrives with the metal, whether the first article is measured rather than assumed, and whether a change to material or process is notified before production rather than after. Those habits are the ones a buyer should probe at the quoting stage, because they cannot be installed later. The quality page of this site is the kind of documentation story to look for.
Which materials should an aerospace component drawing specify, and why does precision matter?
The everyday materials of aerospace custom components form a short list, and each is on the drawing for a reason. Aluminum 6061-T6 carries brackets, housings, and non-structural hardware where machinability and cost rule; 7075-T6 appears where higher strength is wanted. Stainless grades — 304 and 316L for corrosion resistance, 17-4PH in the H900 or H1025 condition for strength — cover fittings and actuators. Ti-6Al-4V is specified where strength-to-weight matters most, and Inconel 718 where the component runs hot. Each is bought against an AMS or ASTM standard, and the drawing should name the standard and the condition rather than the alloy family alone.
Precision in the material callout is what makes the certificate meaningful. "Aluminum" cannot be certified; "6061-T6 plate to the ASTM standard on the drawing, heat number matching the delivered stock" can. When the RFQ names the exact standard and requires the certificate at receiving, it also closes the substitution door — the practice where a stockist quietly offers an "equivalent" grade that is not the grade on the drawing. On aerospace work, substitution without approval is a material change, and the RFQ should say so in plain terms.
What should the material certificate contain, and when should it arrive?
Read a material certificate the way an auditor will read it years later. It must name the specification and condition from your drawing, carry a heat or lot number, and that number must match the marking on the delivered bars, plate, or billet. Where the standard calls for mechanical testing, the certificate should show actual values — tensile, yield, elongation, hardness — rather than a generic statement of compliance. And it must be in English, because it will sit in your quality file and your customer's file after that. A certificate describing a generic grade with no heat number is not a certificate; it is a description.
Timing decides whether the document proves anything. The certificate must arrive with the material and be checked before the stock is cut, because a certificate assembled after machining cannot be tied to the physical metal with confidence. Ask how the shop handles unverified material at receiving — whether it is quarantined until the certificate is checked — and how the shop records which heat went into which work order when one bar or plate feeds several jobs. On aerospace custom components, that heat-to-lot record is the traceability chain, and it is either built as the parts are made or it does not exist.
Where the component is critical enough to justify it, consider requiring positive material identification — an independent verification of the alloy at receiving, such as XRF or PMI testing, in addition to the paper certificate. The certificate proves the material came from a certified heat; a positive identification proves the bar that actually reached the machine matches the certificate. On a substitution-prone alloy or a flight-critical part, that second check closes the gap between the document and the metal, and it costs far less than discovering the mismatch in a finished component.
Which quality system and aerospace flow-downs should a buyer check?
Two certification layers come up when qualifying a custom components manufacturer for aerospace work, and buyers often blur them. The first is the general quality layer: ISO 9001:2015 as the baseline, with IATF 16949:2016 (product design excluded) and ISO 14001:2015 showing additional documentation and process discipline — the factory behind this site holds all three. The second is the aerospace layer: AS9100, the aerospace quality management standard, is held only by organizations certified to it, and the certificate scope names what it covers. Which layer your order needs depends on the component's role and on what your contract flows down.
Flight-critical components under a prime's approved-supplier system normally require AS9100, and the buyer should ask for the certificate and read its scope. Non-flight-critical custom components are commonly made by ISO 9001-certified manufacturers under contractual flow-downs — an AS9102 first article inspection, material and process certificates, traceability, change notification — and this works when the requirements are written down and checked. What never works is a supplier that cannot name its quality system, because none of the records aerospace depends on then have a foundation. Ask for the certificates, read the scopes, and put the aerospace requirements in the contract either way.
What must the first article inspection prove before production runs?
The first article inspection, typically documented to AS9102, is the buyer's strongest verification tool because it proves the shop measured the component rather than assumed it. On a machined aerospace part, the report should document every characteristic the drawing carries: each dimension and tolerance, the geometric callouts such as true position and runout, the surface finish values, the threads, the material and condition, and the drawing notes. For every characteristic the report states the required value, the measured value, the instrument used, and a conformance decision, and a characteristic that does not conform is flagged for disposition rather than corrected silently.
Review the report for the signs of real measurement. A believable report names the instrument for each feature — a CMM for a bore or a true position callout, a profilometer for a finish — and flags non-conformances rather than restating nominal values. Require the FAI before the production run and state in the PO which events trigger a new one: a drawing revision, a change of material source, or a change of process. And look at the photographs of the first article, because the report tells you the numbers and the photo tells you whether anyone actually looked at the component.
Which tolerances are realistic on aerospace custom components, and how are they verified?
On a precision machining floor the capability envelope is well defined. Milling and turning hold ±0.003 mm on controlled features, and where a surface demands more, precision grinding reaches ±0.002 mm as a separate operation. The process capability target on critical characteristics is Ppk ≥ 1.67 initial — the statistical statement that parts sit inside the band with margin rather than at its edge. Both numbers are achievable on aerospace custom components, and both mean nothing until the drawing defines the datum scheme and the measurement conditions.
Two verification rules keep the tolerance story honest. First, separate geometric characteristics from dimensional ones: a diameter can measure perfectly and still be out of round or eccentric relative to its datum, so runout, concentricity, and true position need their own callouts and their own instruments. Second, agree on the measurement reference — dimensional measurement references 20 °C, and aluminum moves roughly 23 micrometres per metre per degree Celsius — and on which instrument verifies each critical feature, because an instrument should resolve about ten times finer than the band it judges. A ±0.003 mm feature belongs on a CMM, not a hand gauge, and the drawing or the PO should say so.
How do heat treatment and surface treatment fit into the component story?
Many aerospace alloys are not used in the as-machined condition. 17-4PH is aged after machining; low-alloy steels are hardened and tempered; aluminum may be anodized; steel may be plated; stainless may be passivated. Each step is a process with a specification, parameters, and records of its own, and each record should reference the same lot as the material certificate so the finished component's story reads as one continuous chain. For the buyer, the questions are who does the treatment and what records prove it: the process specification, the furnace cycle or parameters, and the test results — hardness after heat treatment, coating thickness after plating — all tied to the lot.
Heat treatment also interacts with the tolerance story in a way buyers should plan for. A ground journal or seal diameter is usually ground after heat treatment, because the hardening cycle moves the material and the earlier turning pass cannot be trusted to hold the final dimension through it. That means the process chain on a heat-treated component — turn, heat treat, grind, finish — is also a schedule and a cost chain, and each step needs its own inspection record. When you compare quotes for an aerospace component, compare the process routes as well as the prices: a quote that omits the post-treatment operation is a quote that will grow.
Surface treatment deserves the same documentation discipline. Where anodizing, plating, or passivation is specified, the record should show the process specification and the measured result — coating thickness on a plated thread, for example, which is verified after the coating is applied, not assumed from the bath. Specify the treatment and its acceptance criteria on the drawing, require the process records with the lot, and check them on the first article, because a treatment applied to the wrong condition or thickness is a defect that no dimension report will catch.
Which questions belong on an aerospace RFQ for custom components?
Everything above condenses into a short list that should travel with the first RFQ, so the answers arrive with the price rather than after it.
- Material: Will you procure stock to the AMS or ASTM standard I name, in the condition on my drawing, with the certificate at receiving? May I see a sample certificate format?
- Verification: How is incoming material verified against its certificate before the stock reaches a machine?
- First article: Will you produce an AS9102 first article inspection on the first part and send it for review before the production run?
- Tolerance evidence: For each critical characteristic, which instrument verifies it, and can you provide capability data at Ppk ≥ 1.67 initial?
- Heat treatment and finishing: Who performs the treatment, to what specification, and what process records ship with the lot?
- Traceability: What does the lot record capture — heat number, machine, program revision, operator, inspection results — and in which language? How long is it retained?
- Change control: How are drawing revisions, material source changes, and process changes communicated, and who approves them?
A supplier that answers with named documents and named processes is telling you the truth about its systems; one that answers with assurances is telling you about its sales desk. On aerospace custom components, the certificate, the first article, and the lot record are part of the product, and the buyer who treats them that way gets components that move through the program without arguments.
The buyer's rule of thumb: for aerospace custom components, the material certificate, the process records, and the first article report are deliverables with due dates — exactly like the parts. If a supplier cannot commit to them in the quotation, the quotation is incomplete.
Frequently Asked Questions
Can a custom components manufacturer really meet aerospace requirements?
Yes, when the requirements are written into the order. Certified manufacturers buy traceable stock, verify it at receiving, hold heat and process records, and produce first article reports on request. The verification step never changes: ask to see the documents for one completed order and check that the heat number, certificates, and inspection record line up.
Is AS9100 required for every aerospace component?
No. Flight-critical hardware under a prime's approved-supplier system usually requires AS9100 with a verifiable scope. For non-flight-critical components, ISO 9001:2015 plus contractual flow-downs such as AS9102 first article inspection and material certificates is the common and workable arrangement.
Which materials are common for aerospace custom components?
Aluminum 6061-T6 and 7075-T6, stainless grades including 304, 316L and 17-4PH, low-alloy steels, Ti-6Al-4V, and Inconel 718, each bought to the AMS or ASTM standard on the drawing with the certificate tied to the heat at receiving.
What tolerances can a custom component shop hold?
Milling and turning hold ±0.003 mm and precision grinding reaches ±0.002 mm, with process capability Ppk ≥ 1.67 at the initial study on critical characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. Geometric callouts such as true position and runout carry their own requirements and need CMM-level verification on the first article.
What is the difference between AS9100 and AS9102?
AS9100 is the aerospace quality management system certification a company holds. AS9102 is the standard that defines the first article inspection report — the form and content of the document proving the first part meets every characteristic on the drawing.
Do I need a third-party inspection for aerospace components made in China?
Not always. A rigorous review of the first article, the material and process certificates, and agreed pre-shipment evidence covers many programs. For flight-critical components, or a first order from a shop you cannot visit, an independent inspection before the balance of payment is a reasonable gate.
Need a custom component manufacturer that will put the documentation in the quote?
Send the drawing, the material standard, and your documentation requirements through the contact page — the review will come back with the material, process, tolerance, and record plan stated in writing.