
- XRF material verification on every incoming lot against the mill certificate.
- Ppk ≥ 1.67 initial on key characteristics — a measured chart, not a claim. ±0.003 mm CNC milling, ±0.002 mm CNC turning; ±0.002 mm grinding, verified on CMMs.
- Batch traceability — every part tied back to its raw material and process.
How is the material verified, not just assumed?
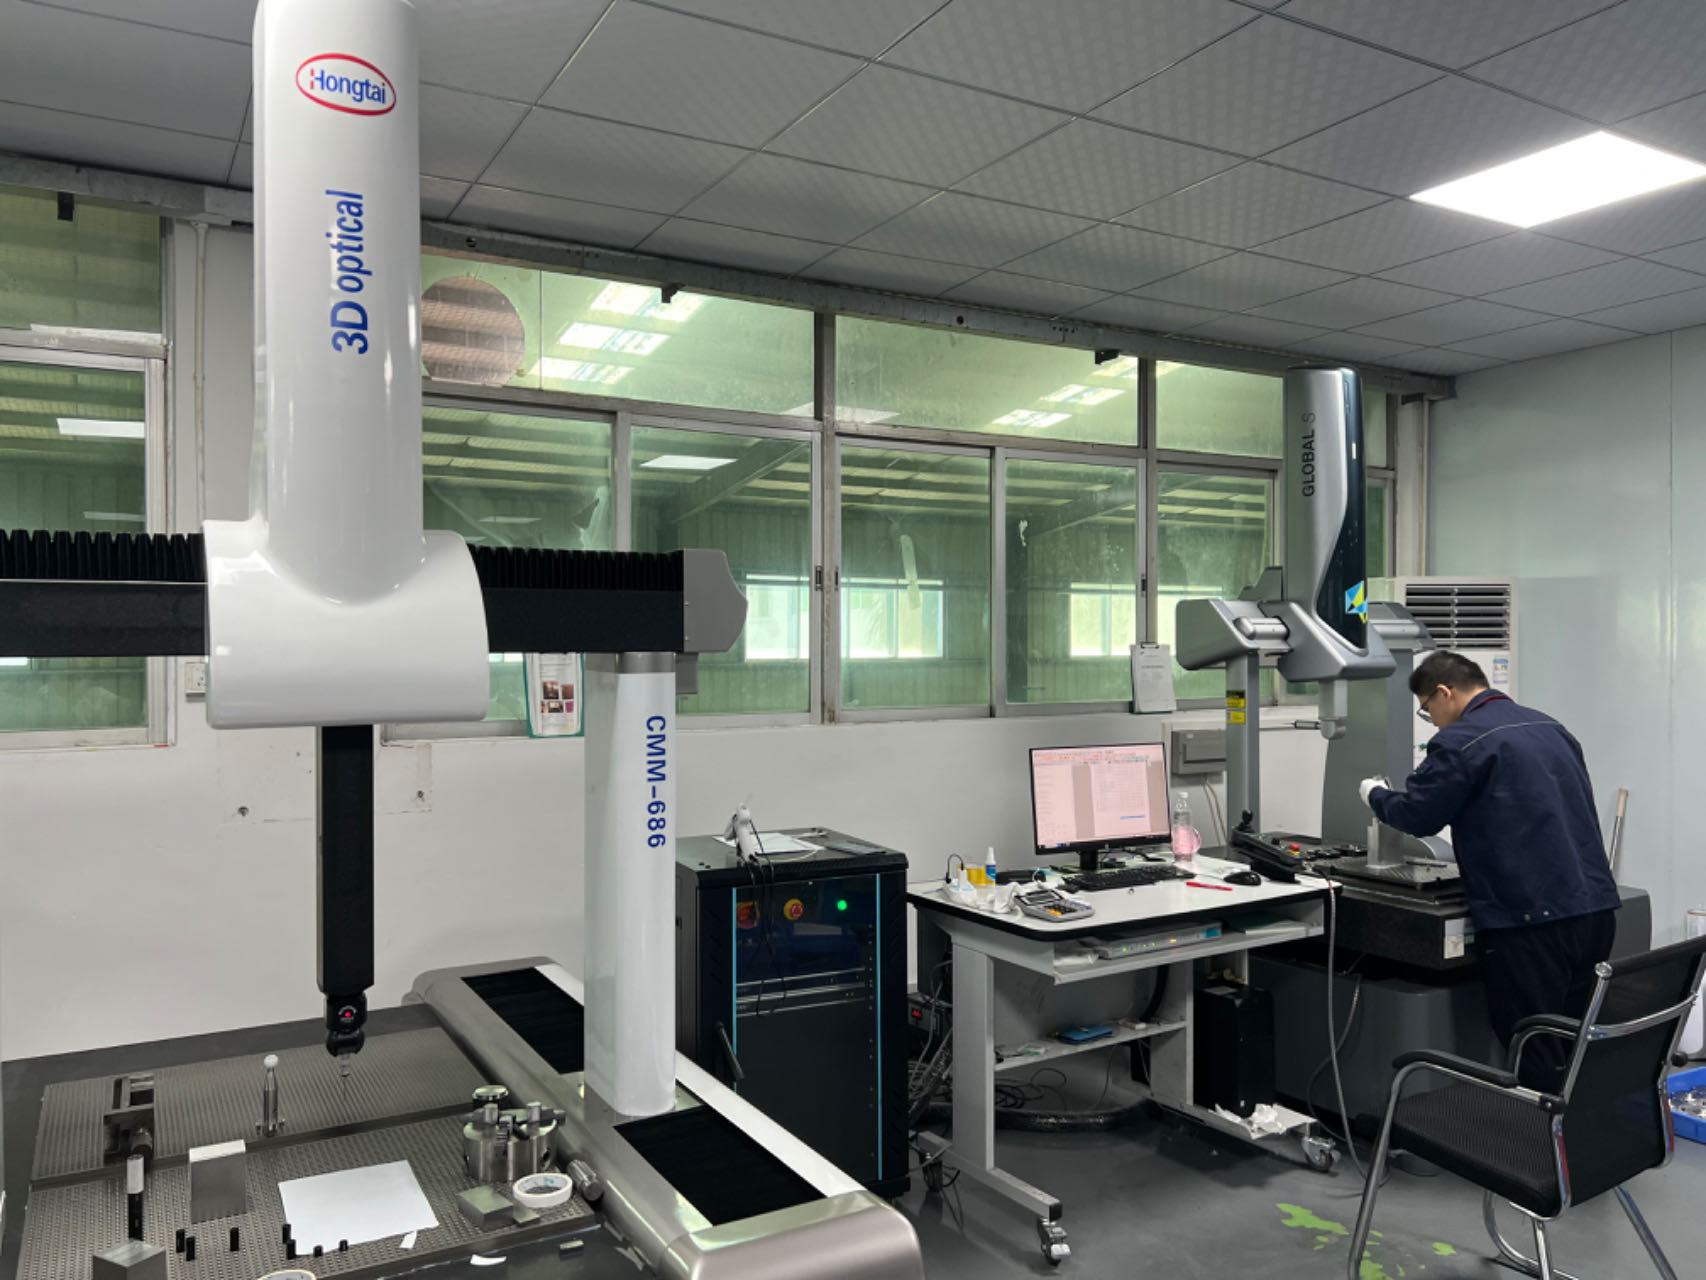
Material is the first thing a component's quality depends on, and the quietest place for a failure to hide. Every incoming lot is checked by XRF spectrometer against its mill certificate before it reaches a machine. The mill certificate states the alloy; the XRF confirms the composition. A substituted or mixed lot is caught at the door, before it has been machined into a thousand parts — the material is verified, not assumed.
The reason the check sits at the door is that it is the cheapest point in the whole process to catch a wrong alloy. Once a substituted bar has been machined into parts, the failure is indistinguishable from any other — it looks right, but it fails in service, and no amount of dimensional inspection recovers a wrong material. The XRF reads elemental composition in seconds, so a 6061 lot is told apart from a 7075 lot, and a 303 lot from a 304 lot, before either reaches a spindle. The material half of quality is won or lost in that one check.
How are dimensions verified?

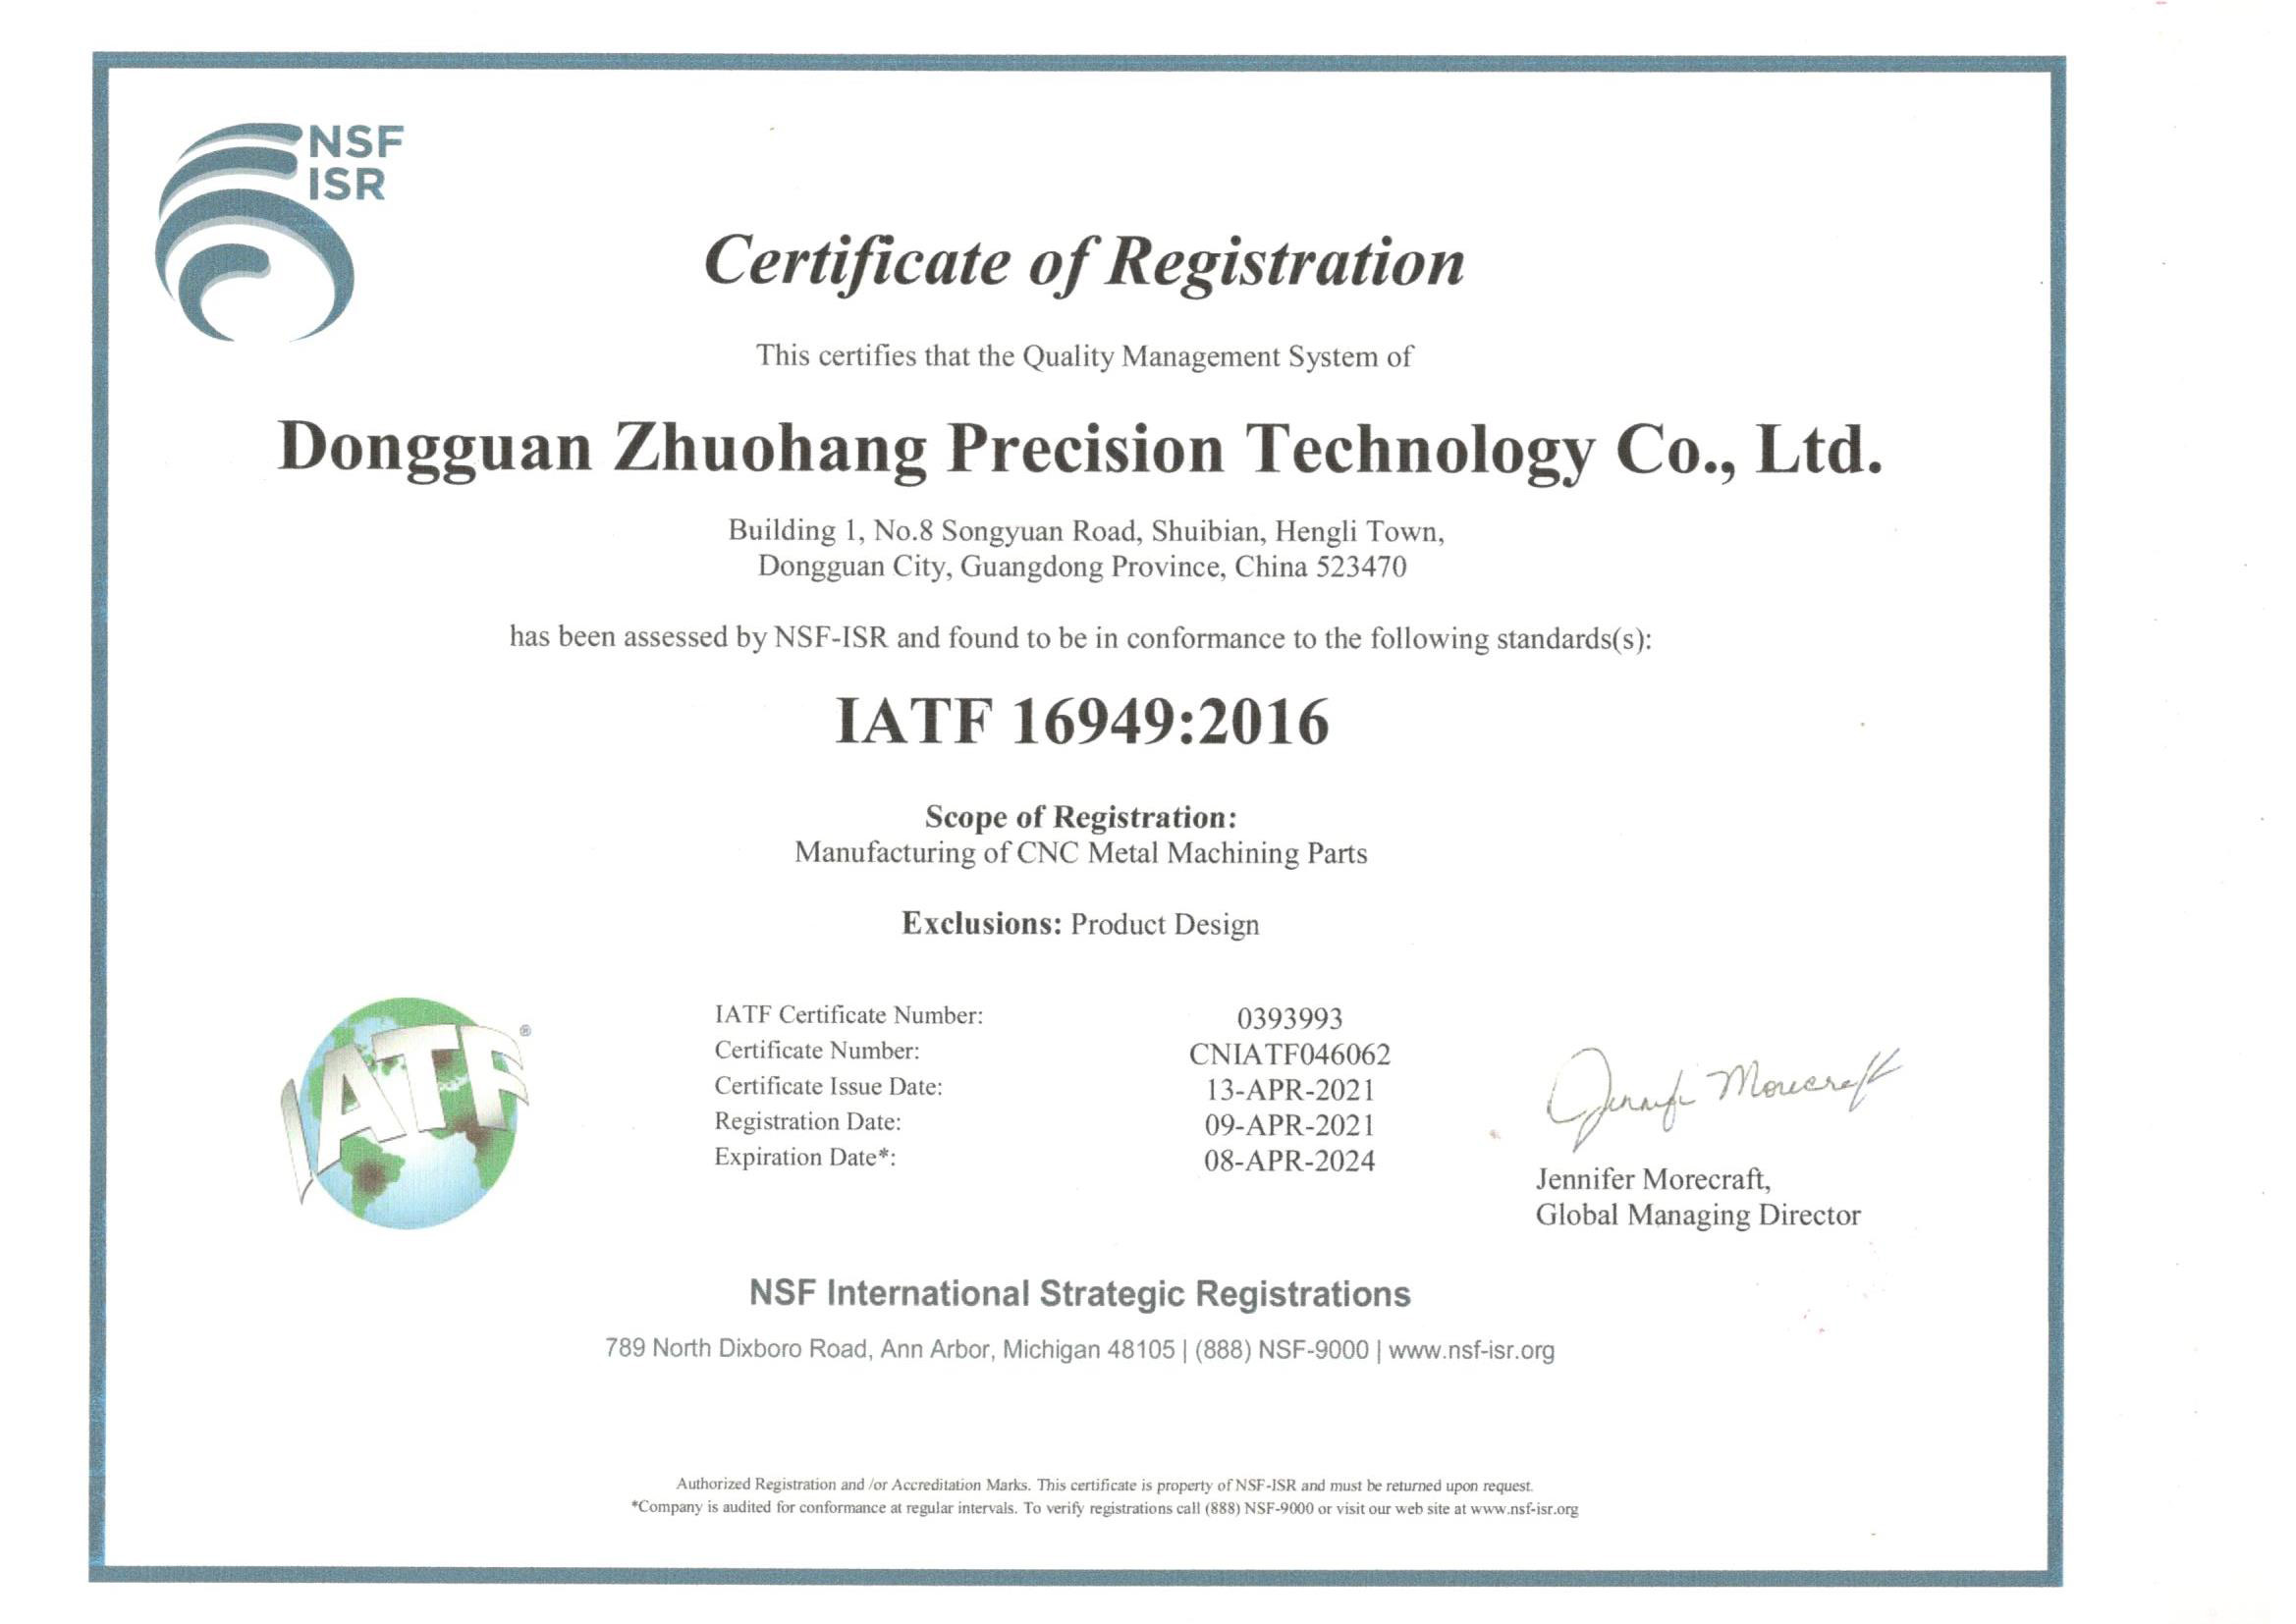
A dimension that is not measured is a hope, and hope is not a quality system. Dimensions are verified on Hexagon GLOBAL S CMMs, vision measuring machines, and a gear measuring center, with ±0.003 mm on CNC milling, ±0.002 mm on CNC turning and ±0.002 mm for grinding. Every critical dimension is measured against the drawing, and the measurement record ships with the part.
| Process | Held tolerance | Verification |
|---|---|---|
| CNC milling | ±0.003 mm | Hexagon GLOBAL S CMM |
| CNC turning | ±0.002 mm | Hexagon GLOBAL S CMM |
| Precision grinding | ±0.002 mm | CMM plus surface-finish / profile instruments |
The CMM is the workhorse because it measures a dimension against the drawing's datums, not against a hand gauge's convenience. The vision machine and gear measuring center extend that to features a touch probe cannot reach — fine holes, gear teeth, profiles. The result is not a pass/fail stamp but a report of measured values, which is what lets a buyer verify the dimension remotely instead of trusting a promise.
What process capability does the shop hold?
Process capability is the number that tells you the process is in control, not just passing individual parts. Key characteristics are held at Ppk ≥ 1.67 initial, general characteristics at Cpk ≥ 1.33. On a representative length characteristic, the SPC records Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) — a measured chart from a real job, with subgroups and a measured mean and range. That is the evidence that a dimension is held by a controlled process, not by luck on a first article.
One more check on that number: the 0.4 mm band behind it is wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright, so read this figure as evidence about one characteristic on one run, not as a blanket tolerance claim.
Cpk is the distance between the process spread and the tolerance band, and it is the honest way to state capability: it tells you not just that a part passed, but how much room the process has before it fails. A Cpk of 1.67 means the process spread fits well inside the tolerance with margin; a Cpk below 1.33 means the process is drifting toward the limit. The measured value of 1.67 on a real job is the difference between a capability statement and a capability fact, and it is the number you should ask for, not a slogan.
How does the XRF verification workflow run from receiving to the machine?
The material check is a sequence, not a single gesture. When a lot arrives, it is matched to its mill certificate and the grade on the certificate is confirmed by the XRF spectrometer against the actual bar. The lot is then stored by grade, so a 6061 bar is not racked beside a 7075 bar waiting to be mixed. When the bar moves to the machine, the lot number follows it, and the traceability record connects the bar, the batch, and the part.
Each step closes a gap where substitution can sneak in. The certificate says what the supplier claimed; the XRF says what the bar actually is; the storage-by-grade says the bar did not get mixed after; the lot number says which parts came from which bar. If you ask for the workflow — not just the certificate — you are checking that all four gaps are closed. The material is verified at the door, and then kept verified all the way to the part.
Does the material verification run on every job?
Yes. XRF verification of incoming material runs on every job, not just automotive or regulated ones. The material honesty you needs is not reserved for the customers who audit; it is the default on every lot, from a single prototype to a full production run. That is the difference between a shop that verifies material when it is watched and one that verifies it as a matter of course.
The reason to run it on every job is that a substituted alloy costs the same regardless of the industry. A mislabeled 6061 lot that should have been 7075 fails in service whether you are a garage startup or a regulated OEM — the failure does not check which customer it is disappointing. Reserving the check for the customers who audit is a signal that the shop knows the check matters and only does it under pressure. Running it as the default is the signal that the shop treats the material as the foundation of quality on every part.
How does traceability tie material to part?
Verification is the first half; traceability is the second. The MES/ERP system records raw-material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results for every lot. Any part can be traced back to its raw material and its process, so if a material question ever surfaces, the answer is in the record, not in a guess.
Traceability is what separates a shop that can contain a problem from one that can only react to it. When a non-conformance surfaces, the record points to the exact lot, machine, and operator, so the affected parts can be isolated instead of treating a whole order as suspect. For regulated buyers that traceability is a requirement; for everyone else it is cheap insurance against the costliest failure — the one where you cannot prove which parts are bad and must replace them all. The chain begins with the XRF check and runs through every step to the finished part.
What inspection equipment backs the material and dimension checks?
The inspection bench covers both halves of the quality question. XRF covers the material; Hexagon CMMs, vision machines, a gear measuring center, a KEYENCE laser microscope, and a SURFCOM profile instrument cover the dimensions and finish; micro-Vickers hardness and Fischer coating thickness cover the material and coating properties. Twenty-plus instruments mean verification never becomes the bottleneck.
- XRF spectrometer — confirms alloy composition against the mill certificate.
- Hexagon GLOBAL S CMMs — verify critical dimensions against the drawing.
- Vision measuring machines and a gear measuring center — reach features a touch probe cannot.
- KEYENCE laser microscope and SURFCOM profile instrument — read surface finish and roughness.
- Micro-Vickers hardness and Fischer coating thickness — confirm material and coating after treatment.
The point of the bench is not the equipment count but the reports it produces. A CMM report with measured values, an SPC chart with a computed Cpk, a material certificate matched to an XRF check — those are the documents that turn a promise into a fact, and they are produced on the floor, not promised on the phone. Verification that is close to the machine and fast enough to run is the only verification that actually happens.
What is a first-article inspection, and how does it validate the match?
A first-article inspection is the full check of the first part off a new setup against every dimension on the drawing, and it is where the material-process match is actually tested. The first article is measured end to end, its material is confirmed against the certificate, and the result is recorded before the batch runs. If the match was wrong — the wrong grade, the wrong process, the wrong tolerance — the first article is where it shows, cheaply, instead of in a whole batch.
An MOQ of 1 piece makes the first article an option on every job, not just production runs. Order one part, run the first-article check, and confirm the material, the process, and the dimensions all line up — then scale. The first article is the cheapest insurance you can buy, because a single part that fails the check costs nothing compared with a batch that fails in the field. The first-article report, like the CMM and SPC reports, is a document you can audit, which is the whole point of a quality system that ships evidence rather than promises.
How does SPC turn a pass/fail check into process control?
Pass/fail inspection catches a bad part; SPC catches a process drifting before it makes one. Statistical process control plots measured dimensions over time against control limits, so a trend toward the limit shows up while the parts are still in tolerance. That is the difference between reacting to scrap and preventing it, and it is the reason Cpk is the number you should ask for, not just a pass rate.
The material is part of the SPC story too. A free-machining material holds a dimension in a tighter, steadier band than a gummy alloy, so the control chart stays flat; a hard alloy drifts as tools wear, and the chart shows the drift in time to change the tool. Key characteristics held at Ppk ≥ 1.67 initial and general at Cpk ≥ 1.33, with a representative run at Ppk ≥ 1.67 at the initial study on key characteristics, are the evidence that the process is in control — measured, not claimed. That is process control, and it is the difference between a shop that inspects quality in and one that builds it in.
Which certifications back the quality system?
Certification means the verification is documented and third-party-surveilled, not ad hoc.
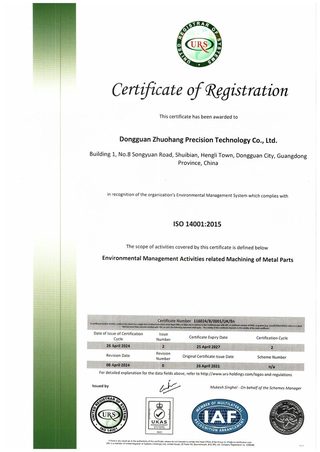
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3 — a build-to-print operation, which keeps the material and design responsibilities unambiguous.
How do you audit the material and dimension verification from a distance?
Request three things: the XRF material verification record for a recent lot, a CMM report or SPC chart from a real job, and the traceability record that ties the two together. A supplier that returns all three is one whose quality claim you can count on; a supplier that hesitates is one whose material and dimension honesty you should question. The verification is documented, so it can be reviewed remotely.
The three documents together are the complete quality story: the material is confirmed, the dimension is measured, and the two are tied to the same lot. A supplier that can produce all three on demand is one whose system is real and running; a supplier that can produce a certificate but not the records behind it is one whose quality lives on paper. The remote audit costs nothing to run and it separates a documented system from a slogan in about as long as it takes to open an email.
How do ISO 2768 and tolerance classes fit the quality system?
ISO 2768 assigns general tolerances to dimensions that carry no individual call-out, in classes from fine to very coarse. It is the clean way to keep a drawing readable: only the features that matter get a tight tolerance, and everything else rides at a stated general class. The quality system then has two jobs — hold the tight call-outs to Ppk ≥ 1.67 initial and hold the general class without spending inspection effort on dimensions that do not earn it.
The connection to the material is direct. Every tight call-out is a dimension that must slow down, and on a gummy material it slows down more than on a free-machining one. A drawing full of tight call-outs on a hard alloy is a quality plan that costs more than the function returns; a drawing that sets the general class deliberately and tight-calls only the critical features is one where the quality effort goes where it earns its keep. The tolerance scheme and the material choice are one decision, and the quality system is what enforces both.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Made for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Made for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Made for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Made for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Made for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Verify the material and dimensions on your component.
Send your drawing to [email protected] or call +86 13126536955 for XRF and CMM evidence from a real job.
Frequently Asked Questions
How is the material verified, not just assumed?
In short, Every incoming lot is checked by XRF spectrometer against its mill certificate before it reaches a machine. The mill certificate states the alloy, the XRF confirms the composition, and a substituted lot is caught at the door — the material is verified, not assumed.
How are dimensions verified?
Dimensions are verified on Hexagon GLOBAL S CMMs, vision measuring machines, and a gear measuring center, with ±0.003 mm on CNC milling, ±0.002 mm on CNC turning and ±0.002 mm for grinding. Every critical dimension is measured, not taken on faith.
What process capability does the shop hold?
In short, Key characteristics are held at Ppk ≥ 1.67 initial and general characteristics at Cpk ≥ 1.33. On a representative length characteristic the SPC records Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) — a measured chart from a real job, not a capability statement.
How does traceability tie material to part?
The MES/ERP system records raw-material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results per lot. Any part can be traced back to its raw material and its process.
Which certifications back the quality system?
ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En). IATF 16949 excludes product design under Clause 8.3 — a build-to-print operation.
Does the material verification run on every job?
Yes. XRF verification of incoming material runs on every job, not just automotive or regulated ones. The material honesty you need is not reserved for the customers who audit — it is the default on every lot.
Custom Components Quality — Related Pages
Continue reading: Custom Components Factory · Custom Components Services · Custom Components Parts Manufacturer
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- IATF 16949:2016 — Automotive quality management system standard